Who owns the tooling
A mould or pattern paid for by you should be yours, and that includes being able to move it to another shop. We put it in writing before the tooling is cut, because afterwards is too late.
What we can help you buy on 1688
Last updated
Castings carry a one-off tooling cost, which changes the arithmetic completely: the first piece is expensive and the hundredth is cheap. Deciding the process is therefore the first real decision.
The second is porosity — gas voids inside the metal that appear when a face is machined and cannot be repaired.
Request a quote for cast housings and structural parts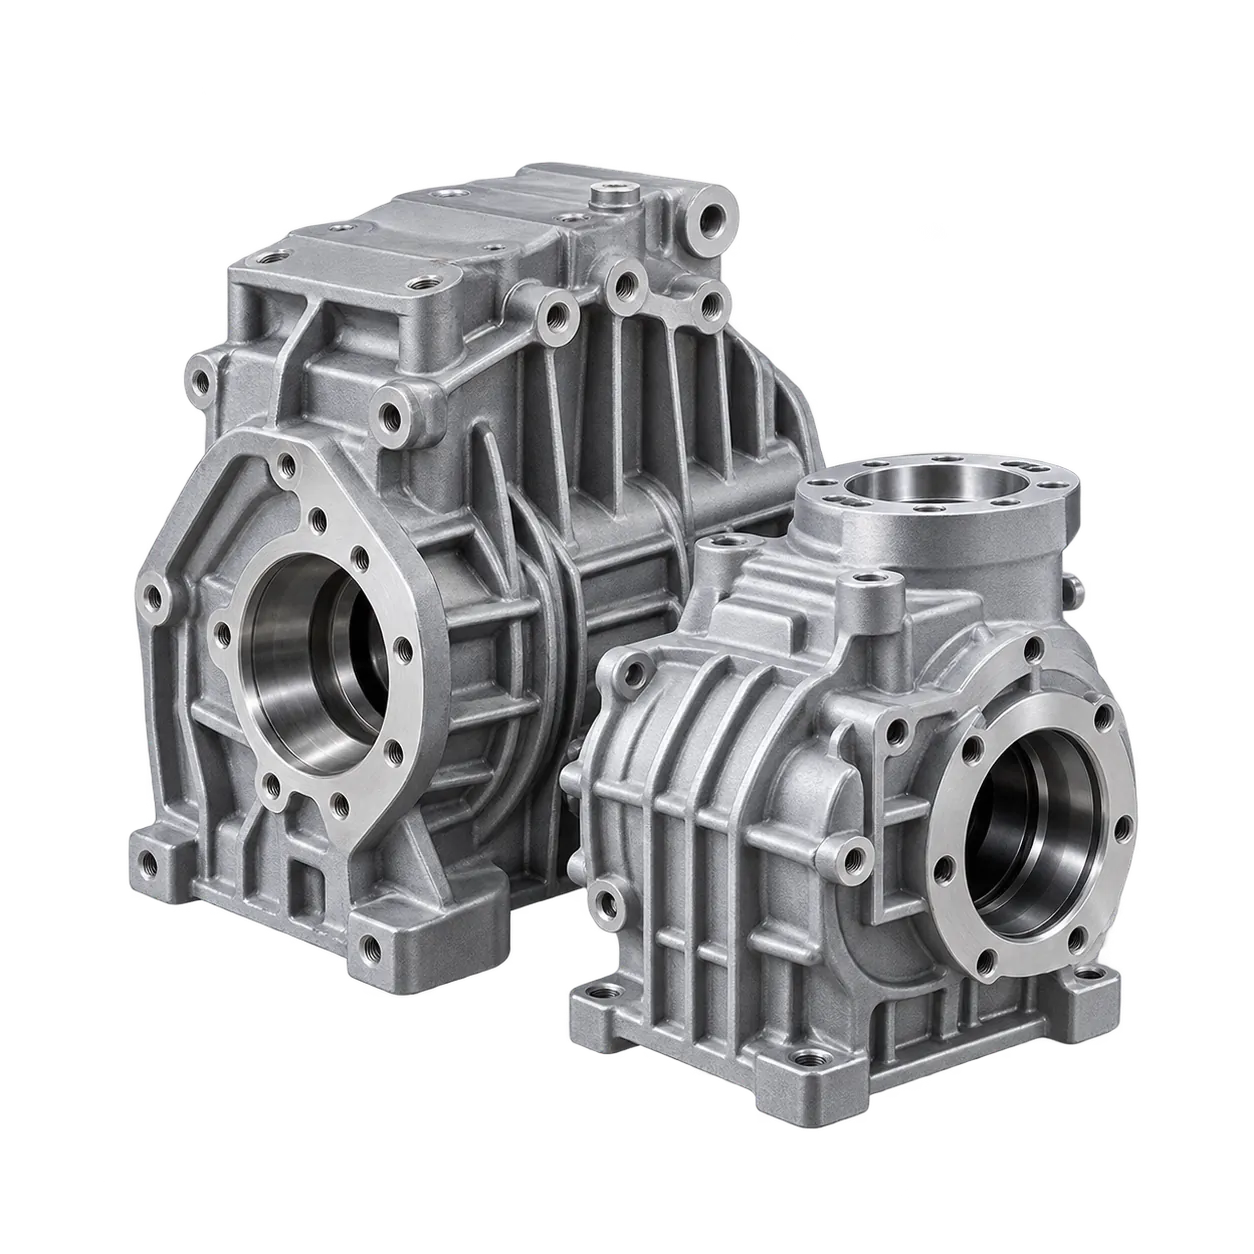
A mould or pattern paid for by you should be yours, and that includes being able to move it to another shop. We put it in writing before the tooling is cut, because afterwards is too late.
Sand, gravity die, high pressure die casting and investment casting differ in tooling cost, minimum quantity, surface finish and achievable wall thickness. The right answer depends on your volume as much as your part.
Cast alloys vary widely in strength and machinability. We ask for the specification and the material certificate rather than "aluminium".
Gas voids inside a casting surface when a face is machined or a part is pressure tested. For anything that holds pressure we specify testing rather than hoping.
A casting that will be machined needs stock left on the right faces and clear datums. Getting that wrong scraps the casting at the machining stage.
For a welded frame, the weld procedure and whether the welders are qualified matter more than the steel. We ask, and we say plainly when a shop cannot answer. A load-bearing part supplied into the EU as a safety component carries requirements of its own.